How should multiple assemblies be organised?
Give each a drawing reference, material and thickness record, weld location and quantity, with access and presentation differences identified.
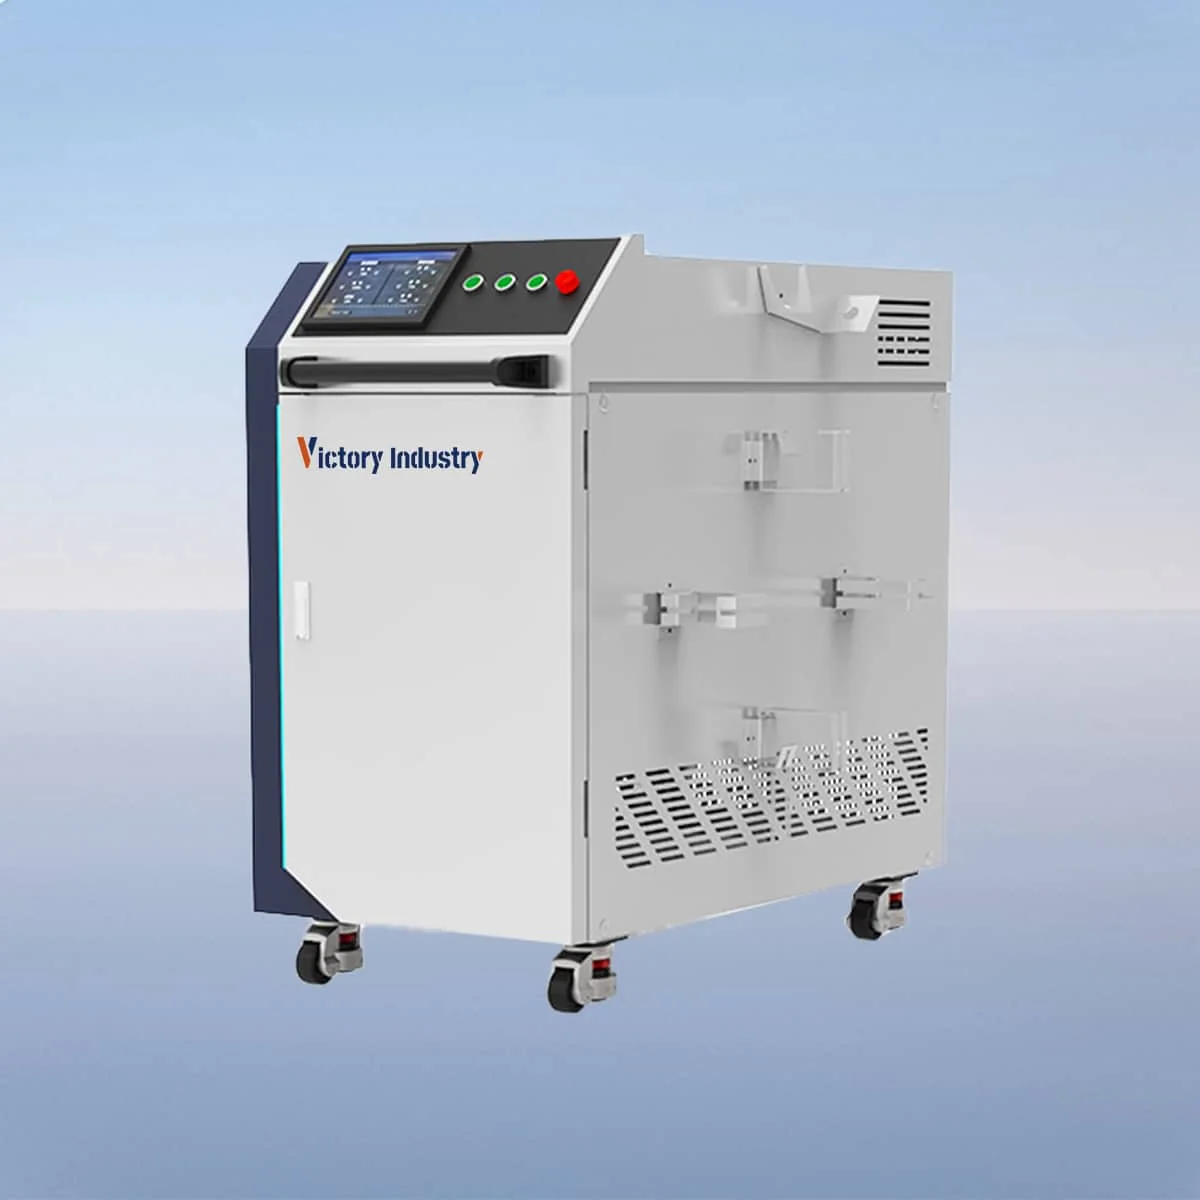
Laser Welding Machine
VIW3000D welding application configuration should define which assemblies belong in the proposed purchase. Give each joint its own drawing and material record, then distinguish current required work from later possibilities. This lets a quotation address a finite application list rather than seeming to confirm every task associated with a high-power model.
VIW3000D is listed at 3000W and 1080nm in the VIW-D handheld welding range. The series describes a movable wheeled structure, generator, industrial water chiller and double-swing welding head. The head has described dual-axis movement; this does not turn the equipment description into a robot or automated-line specification.
| Specification | VIW3000D |
|---|---|
| Laser Power | 3000W |
| Laser Wave Length | 1080nm |
| Laser Source | Raycus, JPT, IPG, Max |
| Fiber Length | Standard 10m, Maximum Support 20m |
| Cooling Method | Water Cooling |
| Support Language | English, Chinese, Japanese, Korean, Russian |
| Working Humidity | <70% No Condensation |
Configuration options vary by model. Confirm the final specification, selected components and operating requirements with your quotation.
A VIW3000D joint project brief should identify the joined parts, materials, thicknesses, weld locations and quantities for each assembly. Keep drawing revisions visible. Where access or part presentation differs between jobs, record those differences even if the material and nominal joint design appear similar.
VIW1500D is listed at 1500W compared with VIW3000D at 3000W. This is a power-rating comparison. It does not demonstrate twice the welding speed, a specified penetration depth or suitability for every thickness in the project. Put the actual joint information beside the comparison.
The VIW-D control description includes setting and monitoring welding parameters, with adjustment of power, speed and focus. These functions and the double-swing head are equipment features to discuss against each job. They do not establish a common procedure or a verified result across unrelated assemblies.
VIW3000D equipment options should address the essential current joints first. Label incomplete geometry or undecided materials as provisional. A component selection should not be treated as confirmation of application details that have not been supplied, or as a guarantee that every weld location is reachable.
Describe the intended positions of equipment and workpieces. Fiber Length is listed as standard 10m with maximum support of 20m. Confirm the offered length and discuss the required arrangement directly, instead of assuming the maximum-support figure is included or proves access to every assembly.
Set out fixture and handling responsibilities for the jobs that need different presentation. Identify buyer-provided items and points that require a response in the offer. The movable machine and dual-axis head descriptions do not imply that a complete part-positioning system or unattended production line is supplied.
VIW3000D quotation requirements should name the chosen Raycus, JPT, IPG or Max source, supplied fiber and water-cooled configuration. Ask for the head, chiller and included equipment to be listed explicitly. Keep this package description tied to the current set of joint drawings rather than a general list of possible applications.
The listed interface languages are English, Chinese, Japanese, Korean and Russian, and Working Humidity is below 70% with no condensation. State the destination and request the applicable setup and installation information. These entries are equipment references, not a promise of support in every language or environment.
Close the comparison with the selected components, supplied items and outstanding application questions in one record. The series and lower-power comparison model provide published context. Send the contact page the current joint list with later applications clearly separated, so the proposal can identify the work it addresses.
Give each a drawing reference, material and thickness record, weld location and quantity, with access and presentation differences identified.
It is the listed laser power. The comparison with 1500W does not establish a proportional welding speed or a penetration result.
It applies to the double-swing welding head, not to a robot-axis count or a complete automated system.
Confirm the actual supplied length. The table states standard 10m and maximum support of 20m.
Keep the current joint requirements, fixture responsibilities, equipment layout and unanswered access or installation questions with the offer.
Compare VIW-D Laser Welding Machine models
Share your material, dimensions and process. Start a conversation about the right configuration.